

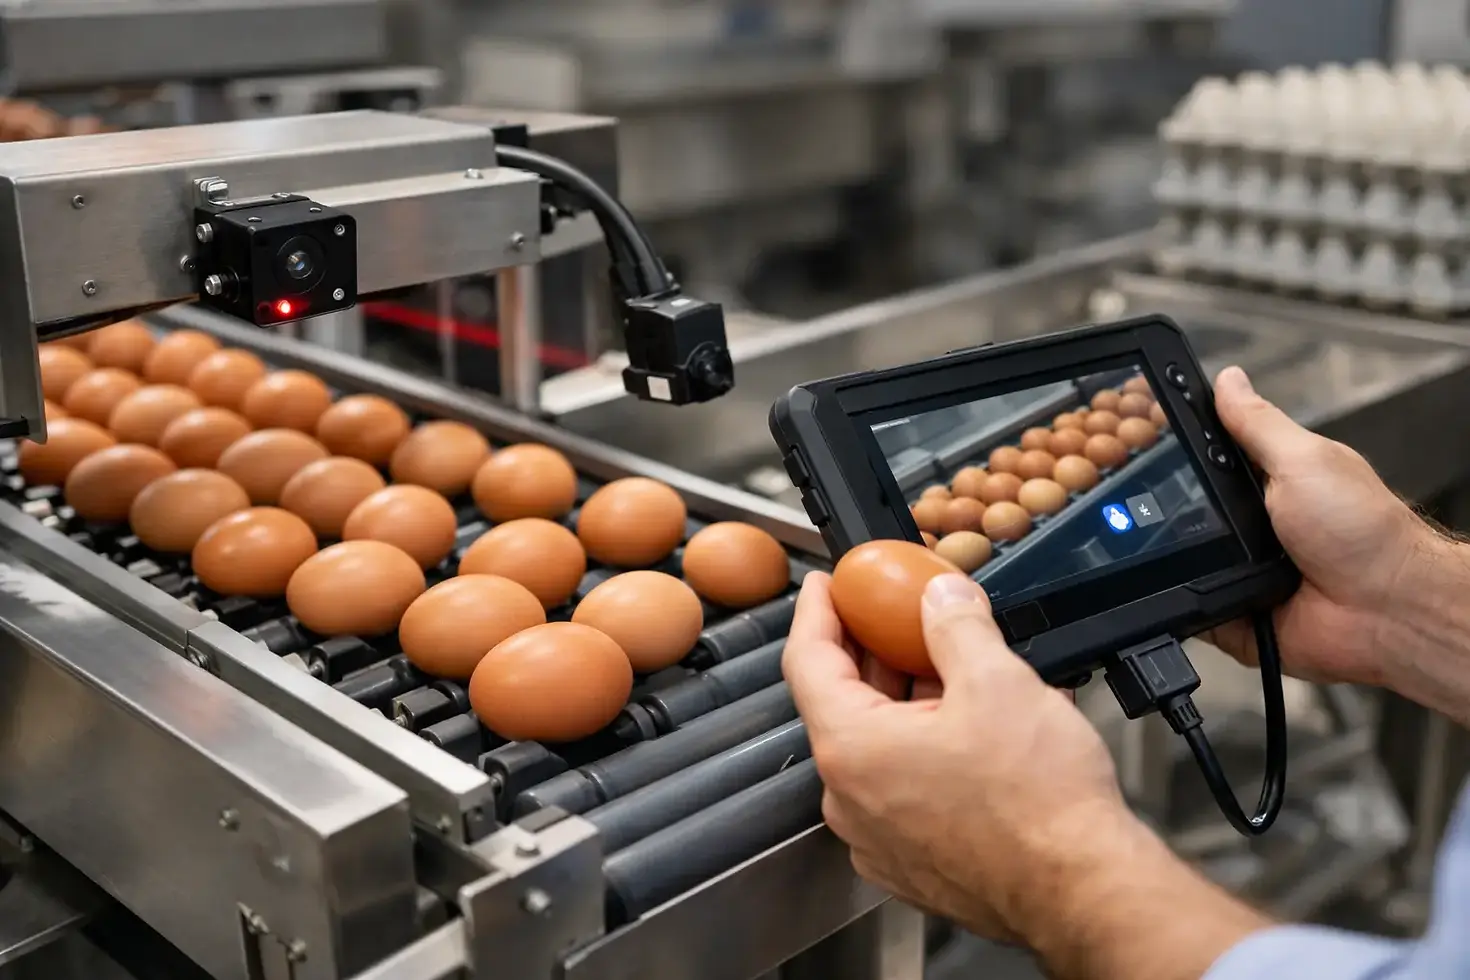
How to Test Egg Counter Output on a Live Line
- bay7962
- Aug 8
- 5 min read
A counter can appear to be working while the production figures are still wrong. The practical way to test egg counter output is to compare a known number of eggs passing through the sensing area with both the counter display and the pulse total received by the farm management system. Test the complete path, not only the sensor.
For a commercial collection line, a meaningful test must reflect normal belt speed, egg spacing, conveyor condition and the output device that receives the count. A bench check has value after installation or repair, but it cannot prove performance under live operating conditions.
Start with a defined test batch
Use a batch of eggs that has been physically counted before it reaches the counter. A batch of 100 eggs is suitable for a basic functional test; 500 or 1,000 eggs provides a better indication of accuracy on a commercial line. Record the verified batch quantity, the date, line identification, belt speed or operating condition, counter reading at the start and finish, and the pulse total if it is available.
Run the batch through the conveyor without manually handling eggs near the sensing area. Intervention can change egg spacing and create a test condition that does not represent normal collection. The displayed increase should equal the known batch quantity. If the counter sends one pulse per egg, the receiving PLC, data logger or farm management input should also increase by the same number.
Where eggs are collected continuously, use a controlled start and end point. For example, mark the first and last egg in a counted group, then confirm the change in the counter total between those two points. Do not rely on a timed sample unless the belt loading is stable and the eggs have been independently counted.
Check the output at both ends
An accurate local display does not automatically mean that the external count is correct. The counter may detect every egg while a loose terminal, incorrect input configuration or electrical interference prevents pulses from reaching the receiving equipment.
Check the counter output at the terminals first, then check the total recorded by the receiving system. Depending on the installation, this may involve viewing a PLC input indicator, examining an input counter register or using suitable electrical test equipment to confirm that pulses are present. Follow site electrical isolation procedures before opening panels or altering connections.
The output type and required pulse duration must match the input device. A PLC input that filters short pulses, for example, may miss counts even when the egg counter is operating correctly. Confirm the input specification, pulse width requirement, voltage level, common reference and wiring arrangement against the equipment documentation.
How to test egg counter output under normal load
Once the basic batch test passes, repeat it while the line is operating at a representative production rate. Egg counters work in the real conditions created by the belt: eggs may arrive in rows, unevenly spaced, rotating, dirty or close to adjacent eggs. A test performed only with neatly separated eggs may fail to reveal an installation or conveyor issue.
Run at least three measured batches at normal speed. Compare each result with the known quantity and calculate the difference:
`Count difference = recorded count - verified egg quantity`
A repeated difference in the same direction points to a systematic cause. Repeated under-counting can indicate an obstructed sensing path, an incorrectly positioned counter or eggs travelling outside the intended detection area. Repeated over-counting can indicate vibration, unsuitable sensor alignment, electrical noise or a mechanical condition that presents an egg more than once to the sensing system.
If results vary from one run to the next, look first at the conveyor rather than changing electronic settings. Belt tracking, bounce, egg accumulation, damaged guides and inconsistent transfer points can all alter how eggs pass through the sensing zone.
Test across the full conveyor width
A two-dimensional infra-red counter is selected to cover a defined belt width. Testing only the centre of the belt is not enough, particularly on wider collection conveyors. Move measured egg groups through the left, centre and right sections of the available counting width, while maintaining normal travel direction and speed.
This check identifies edge conditions caused by poor mounting position, a belt that has drifted from its intended path or guide rails that direct eggs outside the effective sensing field. It also confirms that the counter model is correctly matched to the conveyor. A unit intended for a narrow belt should not be expected to verify a substantially wider egg flow.
For multi-lane or cross-conveyor arrangements, test each transfer condition separately. Eggs may approach the counting point differently after a transfer than they do on a straight belt. The test should include the configurations used during normal collection, not merely the easiest flow pattern.
Inspect the installation before adjusting settings
Most count problems are physical or electrical installation problems. Before altering controls, inspect the counter mounting, belt path and cabling. The sensing faces must be clean and correctly aligned. Dust, feathers, cobwebs and deposits can reduce signal quality, particularly in poultry house conditions.
Confirm that the bracket is secure and that machine vibration has not moved the unit. Check that the belt runs consistently through the designed counting area. A belt that wanders, sags or rises at a conveyor joint changes the egg position relative to the sensor.
Also inspect the cable route. Output cables run alongside motors, variable-speed drives and solenoids can be exposed to electrical interference. Check screening, earthing and terminal tightness in accordance with the site wiring plan. Do not assume that an intermittent output fault is a sensor fault.
The power supply deserves the same attention. Measure supply voltage at the counter during operation, not only with the conveyor stopped. A voltage drop when motors start can cause unstable behaviour or missed communication with downstream equipment. Check polarity and protective devices where applicable.
Separate counter faults from system faults
When the display count agrees with a manual batch but the production software is wrong, the counter is unlikely to be the source of the error. Investigate the interface. Common causes include an input configured for the wrong edge, a scaling value applied in software, an input channel shared with another signal, pulse filtering, or an incorrect reset routine.
Conversely, if both the local display and external system disagree with the manual count by the same amount, inspect the detection and installation conditions. This distinction prevents unnecessary replacement of equipment that is operating correctly.
A useful isolation test is to record three figures from the same batch: the verified egg quantity, the counter’s own count increase and the receiving system’s count increase. The point at which the figures stop matching identifies where the investigation should begin.
Establish an acceptance tolerance and test record
Every site should define what variation is acceptable for its operational use. The right tolerance depends on flock size, reporting requirements, batch size and whether counts are used for day-to-day production monitoring, payment, inventory or automated control. A one-egg discrepancy in a 100-egg diagnostic check has a different significance from a one-egg discrepancy in a full shift total.
Keep a short test record after installation, scheduled maintenance, belt replacement, electrical work or changes to the PLC programme. Record the counter serial number, conveyor location, batch quantity, local count, external count, operating condition and any corrective action. This creates a baseline and makes gradual mechanical changes easier to spot.
Equipment such as the Accucount Mark 5 and Accucount N series is designed to provide a distinct output pulse for each egg, but the result still depends on correct sizing, mounting and integration. The counter, conveyor and control input must be treated as one measurement system.
A controlled batch test at normal line conditions takes little time compared with tracing a day of unreliable production data. Make it part of planned maintenance, especially after work that can alter belt alignment, sensor position or output wiring.


Comments